Overall equipment effectiveness
229
MENTIONS
44
EPISODES
29
PODCASTS
Search complete. 229 mentions across 44 episodes found for "Overall equipment effectiveness".
Oct 30, 2026

Katherine BloughHOST
Not just technically, but intuitively, with the kind of physical familiarity that comes from daily contact with specific equipment over a long time.
Katherine BloughHOST
When the plant deployed its new connected factory platform, real-time OEE dashboards at each work center, production pacing indicators visible to the whole floor, individual operator performance metrics available to supervisors in the management system, Maria was the person whose reaction the plant manager watched most carefully.
Katherine BloughHOST
Because he knew that if Maria decided the new system was something to work around rather than with, the rest of the floor would follow her lead within a week.
Katherine BloughHOST
The first three weeks were difficult.
20 MINS LATER
Katherine BloughHOST
The most effective approaches I have seen share three characteristics.
Katherine BloughHOST
First, they are grounded in operational scenarios rather than the system features.
Katherine BloughHOST
Instead of, here's how the OEE dashboard works, they ask, here's a scenario where your OEE dropped last Tuesday.
Katherine BloughHOST
What does the dashboard tell you? What does it not tell you? And what would you do? Learning to use a system in the context of decisions you actually make is dramatically more effective than learning its features in the abstract.

Mirko PetersHOST
It depends on the definition the plant adopts, and that choice needs to be explicit.
Mirko PetersHOST
If one team excludes changeovers and another includes them, the resulting OEE difference partly describes their calculation choices rather than a difference in how effectively their equipment produces.
Mirko PetersHOST
You're comparing definitions, not performance.
Mirko PetersHOST
Use an approved value applicable to the product and operation, with its effective period recorded.
Mirko PetersHOST
When a machine runs different products during the period, calculate expected production time using the applicable reference for each product before combining the results for the measure.
Mirko PetersHOST
One average cycle time won't capture the real variation.
Mirko PetersHOST
For an OEE measure based on first pass good output, a piece needing rework doesn't count as good on its initial pass, even if the plant later accepts it.
Mirko PetersHOST
The rule needs to be written down and consistently applied.

Alissa DalyGUEST
But plenty of clients are starting at the assessments and kind of roadmap phase.
Alissa DalyGUEST
Plenty of clients are starting with the implementation side of things, taking a look at one line, one OEE pilot, and that's a perfectly good place to start as well.
Matt SoucyHOST
Good perspective.
Matt SoucyHOST
Really kind of gives the full gauntlet of what we're trying to do here.

Casey FlanaganNARRATOR
Hi, I'm Casey Flanagan, Associate Editor with ProFoodWorld.
Casey FlanaganNARRATOR
This AI generated podcast episode covers how food and beverage manufacturers can turn overall equipment effectiveness or OEE from a passive scoreboard into an active driver of plant performance.
Casey FlanaganNARRATOR
It highlights how establishing honest baselines, breaking losses into availability, performance and quality, and using digital tools for real time coaching can shift operations toward continuous improvement.
speaker_2HOST
What if I told you the manufacturing metric that your plant floor is completely obsessing over is actually destroying your productivity?
speaker_3HOST
Yeah, that's a tough pill to swallow, but it is happening everywhere.
speaker_2HOST
So in this deep dive, we're going to explore how digital tools can actually transform overall equipment effectiveness or OEE.
speaker_3HOST
Yeah, moving it from just a static recording scoreboard into an active real-time driver of plant performance.
speaker_2HOST
Exactly.

speaker_0HOST
Where was damage happening in a bottling process? SmartSkin provided the answer.
Kumaran ThillainadarajahGUEST
Before SmartSkin, plants measured the output, OEE, speed of line, container damage, but they never knew what was causing those numbers.
Kumaran ThillainadarajahGUEST
We help them measure container handling.
Kumaran ThillainadarajahGUEST
The initial concept was that we could reduce glass breakage, but reducing glass breakage is the very tip of the iceberg.
Kumaran ThillainadarajahGUEST
It's one application for our technology.
Kumaran ThillainadarajahGUEST
Really, what we do is we help plants understand container handling, which is something that they were never able to do before.
Kumaran ThillainadarajahGUEST
So plants measure OEE, which is operational efficiency, But that's the output of all these other factors.
Kumaran ThillainadarajahGUEST
So they never understood why their OEE was down or what was causing them to damage their

Colin DenihanGUEST
No, when I say autonomy, they have accountability for their P&L.
Colin DenihanGUEST
They have accountability for the OEE numbers.
Colin DenihanGUEST
They have accountability for their quality and accountability on their gross margin.
Colin DenihanGUEST
They are still getting the support from our home corporate office.

Kirsten FailingGUEST
Just really settling in with that and then taking a bead and letting it work for a while.
Kirsten FailingGUEST
The second one to me is OEE.
Kirsten FailingGUEST
So we've tackled several foundational items like our quality rate.
Kirsten FailingGUEST
We did a big project a couple of years ago where we went from like 85% first pass yield and now we're at 96%, which with tight tolerances, we're very proud of.

Aron KolosikHOST
Look at your technology, too, as part of this processes and systems.
Aron KolosikHOST
Is my ERP system giving me what I need? Is my manufacturing excellence system or OEE tracking giving me what I need? You need to assess your processes and your systems.
Aron KolosikHOST
Are they working and not working for you versus what you would expect? from a plant or an operation like yours.
Aron KolosikHOST
So again, working, not working on processes and systems.

Aron KolosikGUEST
We made shampoo, Pantene, and Head & Shoulders back in the day.
Aron KolosikGUEST
And they run 380, 400 bottles a minute on that line, and our job was to drive OEE.
Aron KolosikGUEST
and i remember telling people at that time again as a young leader hey you need to have your head on a swivel like these were literally my words you need to have a head on this well you need to be looking to see where the next thing's going down and get there before it causes the line to go down but what that created was this hustle culture of like we were manhandling the results if you will and so they were they were incredibly reactive so our our time between going down and going back up it was really really short but the problem was we were still going down And when you pull off the energy or the focus, those aren't unsustainable.
Aron KolosikGUEST
And I'm telling people to hustle and move and move faster culturally versus the opposite, which is, hey, let's focus on why are we going down and let's figure out how do we extend the length of the run so you can actually see what happened when you went down and look and observe.
Mirko PetersHOST
Removing uncertain intervals can make the remaining operating period appear better than the full record supports.
Mirko PetersHOST
This becomes particularly sensitive with overall equipment effectiveness, or OEE.
Mirko PetersHOST
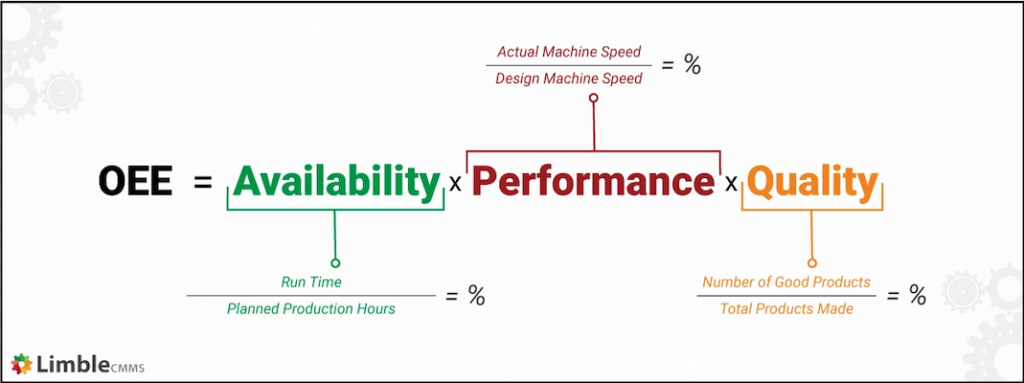
OEE combines availability, performance and quality, and each factor depends on agreed definitions of the time, output and acceptable production included in its calculation.
Mirko PetersHOST
Availability compares operating time with planned production time.
Mirko PetersHOST
Production needs to define which scheduled periods belong in that denominator, including how breaks, planned maintenance and other agreed exclusions affect the time against which availability gets judged.
Mirko PetersHOST
An interruption too short for the collection method to capture can't become a reliably measured microstop simply because the reporting team chooses a threshold that includes it.
Mirko PetersHOST
Quality also needs a defined counting basis.
Mirko PetersHOST
For the OEE calculation, agree which output counts as total production and which output counts as acceptable production.
34 more episodes mention Overall equipment effectiveness.
Create an account to see the whole feed, search across every transcript, and follow the entities you care about.